A Clear Specification Prevents Costly Surprises
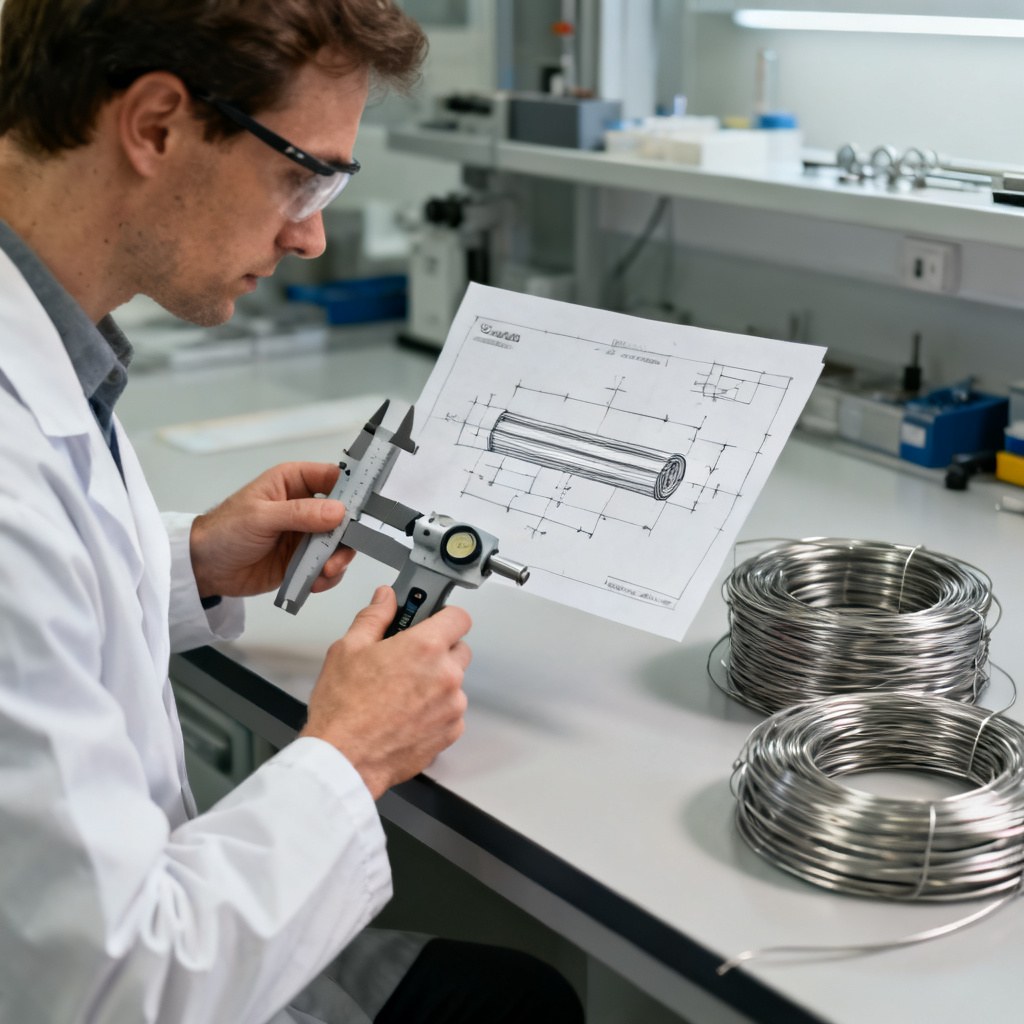
Seal strip steel core problems rarely appear at goods-in. They show up weeks later as sag, poor clamp load, coating flake, or a line stoppage when the coil tangles. Most of these trace back to an incomplete core drawing. The fix is a specification sheet that leaves nothing to interpretation.
What to Define on the Drawing
| Parameter | What to State |
|---|---|
| Material / grade | Carbon, spring temper, galvanized, plated, or stainless, plus strength range |
| Wire diameter | Nominal diameter and tolerance (often ±0.02–0.05 mm) |
| Profile & pitch | Straight, zigzag amplitude and pitch, or U-form channel width |
| Temper | Annealed-soft, or spring temper with target tensile |
| Coating | Type and coating mass (g/m²), adhesion requirement |
| Coil form | Spool or level-wound, coil weight, inner/outer diameter, weld policy |
| Length & packing | Continuous length, protection, labeling, and traceability |
Dimensional and Profile Tolerances
Dimensional control is what keeps clamp load consistent. Typical points to tolerance are wire diameter, profile amplitude and pitch, channel width and opening, and camber or straightness over a defined length. Specify the datum and the gauge method so supplier and customer measure the same way — laser gauging and contact comparison should agree.
Mechanical Properties
- Tensile strength: set a range, not a single value, so the core is strong enough to hold clamp load but ductile enough to form.
- Elongation: confirm the profile bends can be made without coating cracks.
- Temper consistency: lot-to-lot variation is what makes one coil behave differently from the next.
Coating and Surface Requirements
State the coating type, minimum coating mass, and an adhesion test (bend plus tape). For bonded seals, specify the bonding system and require the supplier to demonstrate rubber adhesion after vulcanization. Add a cleanliness note — oil, dirt, and slivers cause bonding failures and feed problems.
Documentation and Standards to Request
For automotive programs, require a quality system aligned to IATF 16949, and ask for the PPAP elements that match the part's risk level: dimensional results, material and performance testing, process flow, PFMEA, control plan, and measurement system analysis. A material certificate and salt-spray report per lot close the loop on corrosion and traceability. Where an OEM specification or a national standard (ASTM, ISO, GB/T, or a customer drawing) applies, cite it directly on the purchase order.
A Short DFM Checklist for Wire Cores
- Is the bend radius achievable for the chosen temper without coating cracks?
- Is the clamp load requirement realistic for the wire diameter and profile?
- Will the coil form feed the extrusion line without tangling or welding stops?
- Is the coating specified for the real service environment, not a generic one?
- Are inspection methods and acceptance limits defined for both sides?
Build the Spec With Your Supplier
The best core specifications are written jointly by the seal engineer and the wire supplier. Hold-Tech reviews seal strip steel core drawings for manufacturability, recommends the grade, temper, and coating that meet your life and line requirements, and supplies to the documentation your quality system needs. Send the drawing to operator@hold-tech.cn or call +86-186-60386138.