What a First Article Inspection Is
A First Article Inspection (FAI) verifies that the manufacturing process — before full-rate production — produces a part that fully conforms to the drawing and specification. It is the supplier's evidence that the process is capable, and it is your first line of defense against a bad production run.
The result is a written report that documents, dimension by dimension, that a representative part matches the print. For aerospace and defense work it is typically produced to AS9102; many OEMs request an equivalent FAI for commercial and industrial parts even when a formal standard is not mandated.
What an FAI Report Contains
- Part accountability: drawing number, revision, material certified to the print, finish, and special process records.
- Characteristic-by-characteristic results: every dimension, tolerance, and note on the drawing, with measured values and pass/fail.
- Material certification: mill test certificate or material cert traceable to the purchase of the raw stock.
- Inspection tools and methods: which gauges, CMM program results, and instruments recorded each dimension.
- Approvals: inspector, review engineer, and (in AS9102) the supplier's quality manager sign-off.
- Nonconformance findings: any characteristic that did not meet print, the disposition (use-as-is, rework, scrap), and the corrective action.
When an FAI Is Required
- First production run of a new part number.
- After any change to design, material, process, tooling, or a major supplier change.
- After a lapse in production long enough that the process was reset.
- When the customer contractally requires an FAI (common in aerospace, defense, medical, and automotive tiers).
How Inspection Methods Differ
A good FAI does not just report values — it uses the right tool for each feature:
| Feature Type | Typical Tooling | Notes |
|---|---|---|
| Outer/inner diameters, critical distances | CMM (coordinate measuring machine) | Programmed for repeatability across runs |
| Small bores, slots | Pin/plug gauges, bore gauges | Fast, reliable for go/no-go |
| Surface finish | Profilometer / surface roughness tester | Ra compared to print callout |
| Threads | Thread plug/ring gauges or optical | Verify pitch, class, and profile |
| Textured/geometric features | Optical or laser scanner for GD&T surfaces | GD&T datum references tracked |
| Hardness | Hardness tester (Rockwell/Brinell/Vickers) | Per material spec zone |
Reading an FAI Report Critically
- Confirm the drawing revision matches your released revision — an FAI on the wrong revision protects nothing.
- Check that every dimension listed on the print appears in the report. Missing characteristics are a red flag.
- Look at the margin, not just pass/fail. A dimension that measures at 90% of its tolerance is a warning that process drift could push it out on the next run.
- Verify material cert traceability matches the heat/lot code claimed.
- Keep the signed FAI as your record — it is the baseline your supplier's process must maintain.
FAI at Hold-Tech
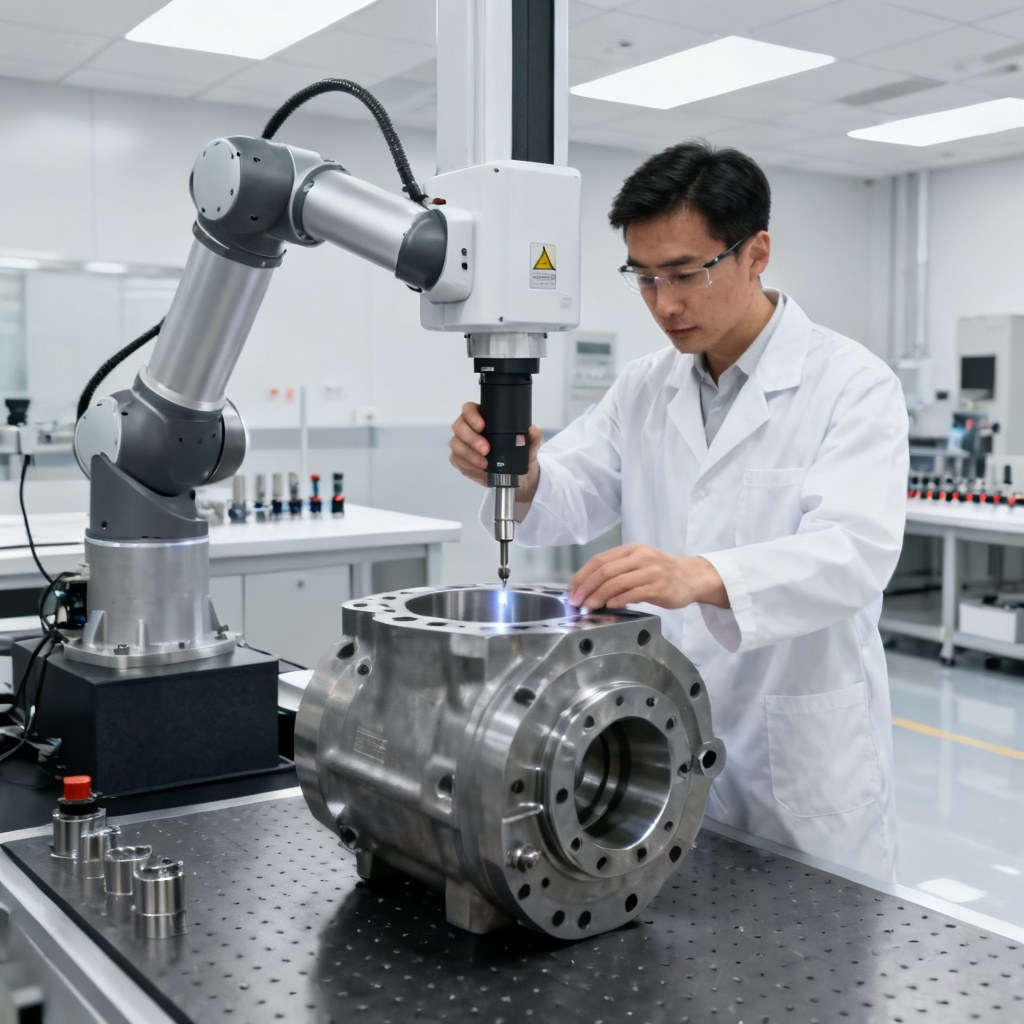
Every production order we machine starts with part accountability review, and our inspectors produce FAI-style documentation with CMM and calibrated gauges for the dimensions that matter. When a drawing carries a tight GD&T scheme, we build the inspection program before the first part comes off the machine so the first article is documented, not improvised.
Request an FAI or FAI-style report on your next machined part by contacting operator@hold-tech.cn — it is the cheapest insurance against a bad production run.