Two Drawings for the Same Part
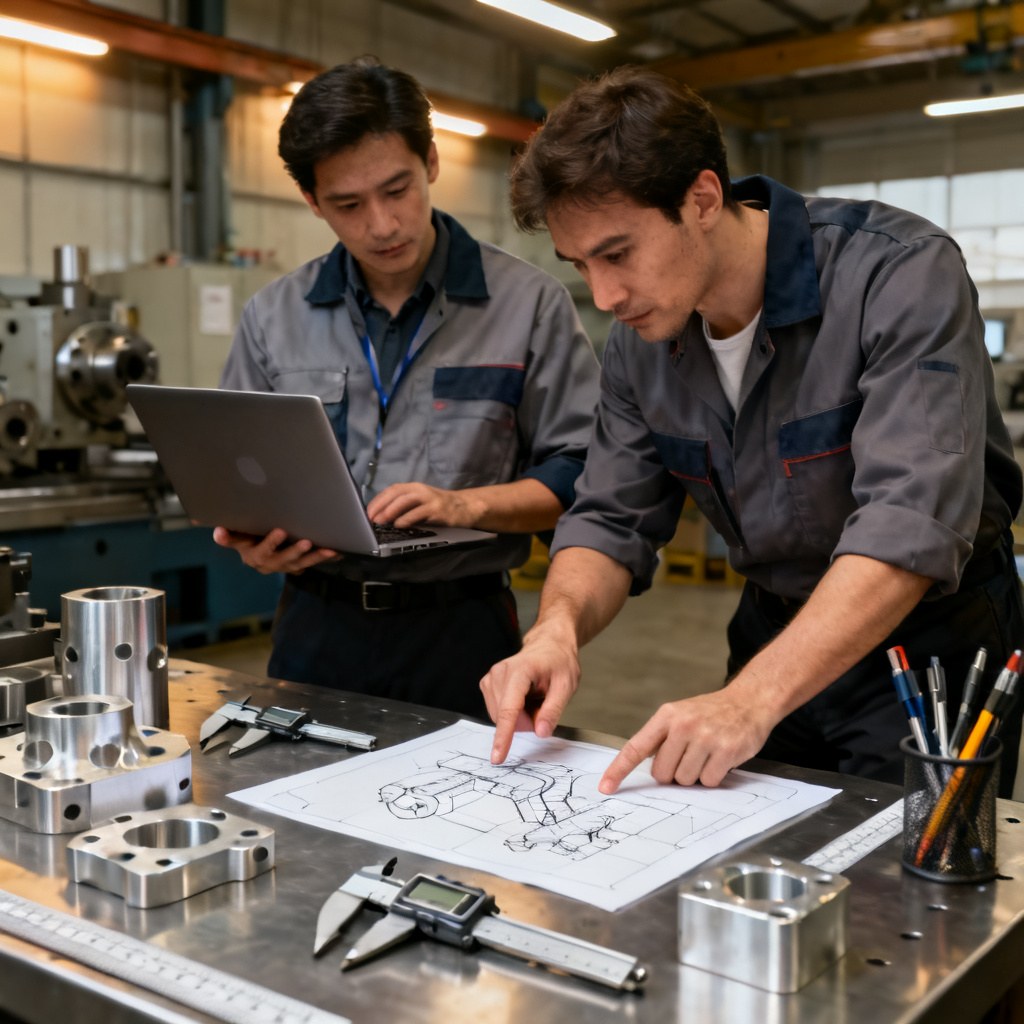
Give the same functional part to two designers and you can get two very different cost outcomes. The part will measure the same and serve the same duty, but one might take twenty minutes of CNC time while the other takes ninety. The difference is not the machine or the shop — it is the drawing. Cost is designed in long before a cutting tool turns.
The Drawing Decisions That Move the Price
| Decision | Costly Version | Cost-Smart Version |
|---|---|---|
| Internal radii | R0.5 corners in deep pockets | R3+ radii made with standard end mills |
| Slot widths | Odd improvised sizes | Widths matched to common tooling |
| Deep features | Pockets deeper than 4× tool diameter | Shallow pockets, stepped bottoms |
| Tolerances | ±0.01 mm on every dimension | Default ±0.1 mm, tight only where function needs it |
| Setups | Features on six faces | All critical faces machined from one or two setups |
| Datum | Dimensioning from three unrelated faces | One primary datum, a secondary, one tertiary |
| Edge treatment | Silence on edges and burrs | Stated deburr, finite break on functional edges |
Say What Matters — and Only That
Every tolerance you call out costs inspection and scrap decisions. When every dimension carries a tight tolerance, the shop cannot concentrate effort or process planning where it matters, and the quote includes the risk of every dimension being scrutinized. A drawing that tightens only the bores, sealing faces, and locating features — and leaves the rest generous — produces faster cycle times, better yields, and a lower price.
Give the Cutter Room
Most avoidable cost comes from geometry the cutting tool cannot reach:
- Corner radii: a standard end mill leaves a radius equal to its own size, so internal corners should be specified at or above common tool radii — R1, R2, R3, R5, R6 — not tight pockets that force small tools and slow feeds.
- Floor radii: specify generous radii at pocket bottoms; a sharp bottom needs a slow pass and a delicate tool.
- Deep holes: keep depth-to-diameter ratios reasonable, and call out peck or interrupted conditions so the shop can plan tooling instead of discovering them.
- Undercuts and fine grooves: these need special tools and extra setups — include them only where function requires, and say so.
Thin Walls and Heat
Thin-wall parts deflect under clamping and machining force, and they distort as heat is generated. If the design demands thin walls, expect deflection: calling out wall thickness, clamping strategy, and a roughing sequence is how a skilled shop keeps the bore round and the flat areas flat. When you can, add a small chamfer or thicker corner for clamping rather than fighting distortion later.
Materials and Stock
Material selection is a cost decision before it is a performance decision. Standard grades of aluminum, carbon steel, and 303/316 stainless are stocked by the shop, are machinable at practical speeds, and need no special tooling. Exotic alloys and high-strength steels slow cutting dramatically, demand coated tools and coolant discipline, and stretch both cycle time and tool cost. If a hardened surface is not needed, leave the part soft.
Standard Threads, Clear Callouts
Specify threads with clear depth, class, and percent-of-thread statements, and they are quick to quote and quick to make. Depth stated as “full thread + drill point + break edge” saves the machinist from guessing. Where a thread will be inspected or must accept a specific fastener, say so — and where a weld or bonded assembly removes the need for a threaded feature entirely, remove it.
A Checklist Before You Release
- Can every feature be reached by a standard tool without special orders?
- Are the tight tolerances strictly the functional ones?
- Is the datum chain simple, with machining that starts from one primary face?
- Can the part be clamped safely in a cycle that respects the machine's capacity?
- Are materials, finishes, edge treatment, and documentation all stated?
Let the Supplier Review Early
The cheapest way to avoid all of this is to share the 3D model, not just the 2D drawing, with your machining partner before the design freezes. A twenty-minute manufacturability review with someone who runs the machines is worth more than a week of rework. Hold-Tech reviews drawings and models for every project before quoting, and tells you where cost can come out without compromising function. Send your part to operator@hold-tech.cn or call +86-186-60386138.