Why Titanium Is Hard to Turn
Titanium alloys such as Ti-6Al-4V are prized for their strength-to-weight ratio and corrosion resistance, which is why they dominate aerospace, medical, and energy applications. But those same properties make titanium one of the most demanding materials to machine on a CNC lathe.
The metal has low thermal conductivity — roughly one-fifth that of steel — so the heat generated at the cutting edge stays concentrated in a very small zone. If it is not controlled, that heat destroys cutting tools quickly and damages the surface of your part. Additionally, titanium's high chemical affinity means it tends to weld itself to the tool edge, a failure mode called part-galling that ruins both the insert and the workpiece.
Tooling Selection That Holds Up
Tooling is the first decision that determines whether a titanium turning job succeeds or fails. At Hold-Tech we prefer carbide inserts with sharp, positive cutting edges and a large approach angle, which reduces cutting forces and keeps heat away from fragile edge geometry.
- Grade Selection: Use micro-grain or fine-grain carbide grades designed for heat-resistant superalloys, often with a PVD coating like TiAlN to resist abrasion.
- Edge Preparation: A light edge hone strengthens the cutting edge without adding excessive cutting force.
- Geometry: Positive rake angles help shear titanium cleanly, and a 45° entering angle spreads the cutting load over a longer edge.
For small-diameter titanium parts, micro-boring bars with a high overhang-to-diameter ratio are prone to chatter. Where possible, we use stub-style toolholders and dampened boring bars to keep vibration out of the cut.
Speeds, Feeds, and Depth of Cut
Surface speed is the main variable that controls tool life with titanium. A common starting point is 30–60 m/min for rough turning with carbide, depending on alloy and rigidity. At these speeds, feed per revolution is typically kept low — around 0.08–0.25 mm/rev — to manage chip load.
Keeping the tool engaged is important. A constant depth of cut prevents the edge from rubbing against hard, work-hardened skin left by the previous pass. We prefer to maintain a minimum depth of 0.20 mm whenever possible so the insert cuts into fresh material rather than burnishing the surface.
Coolant Strategy: High Pressure Wins
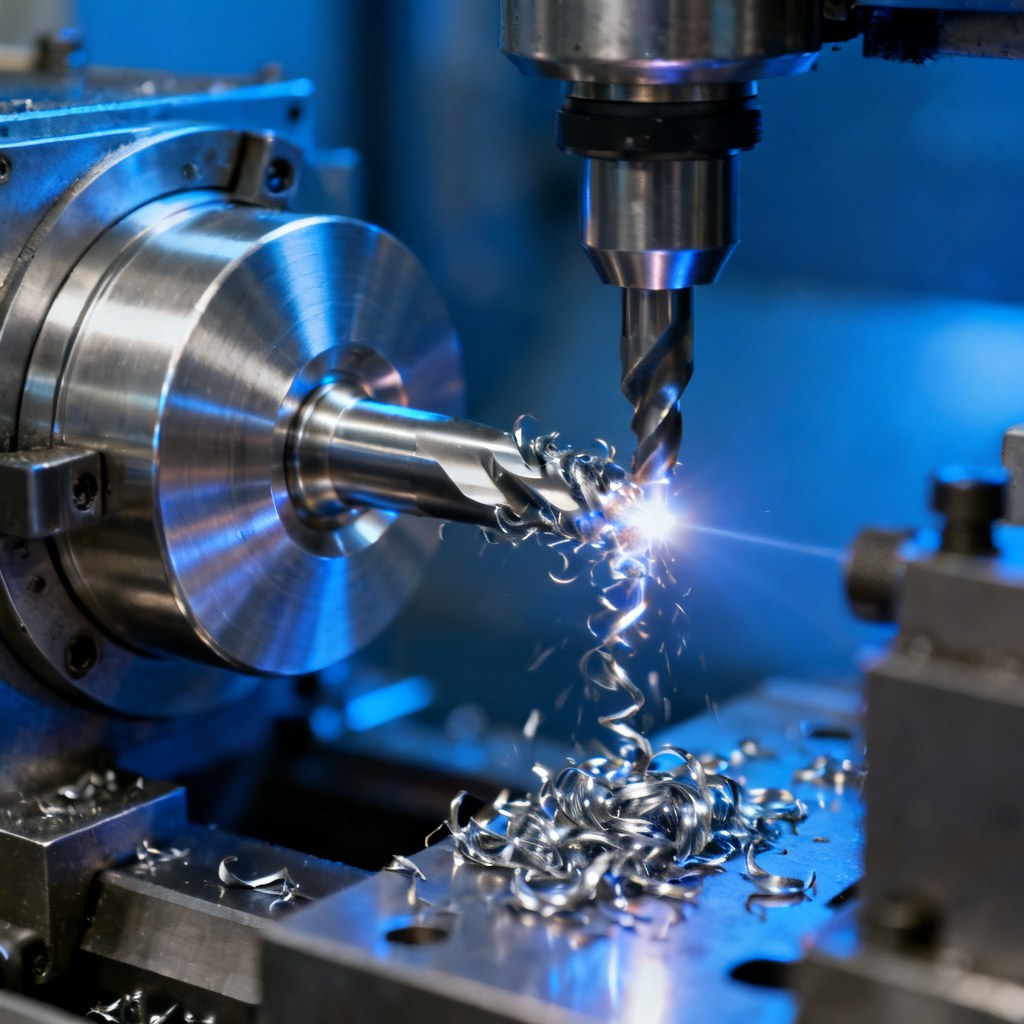
Because titanium traps heat at the cutting zone, coolant delivery is not optional. High-pressure coolant, supplied at 70–150 bar directly at the cutting edge, breaks chips and flushes heat away. It also prevents the small, stringy chips titanium produces from wrapping around the workpiece and creating a safety hazard.
When high-pressure systems are unavailable, we increase coolant volume and direct both the main and secondary nozzles precisely at the tool–workpiece interface. Flood cooling alone rarely removes enough heat for sustained titanium production.
Holding Tolerances and Surface Finish
For tolerances around ±0.01 mm, thermal expansion of the workpiece and machine both matter. Letting the part cool intermittently before final passes allows the dimensional readings to stabilize. We measure titanium parts at a controlled temperature and re-cut only after readings confirm the part has stopped moving.
For surface finish, the feed rate, tool nose radius, and depth of cut come together. A larger nose radius improves finish but increases radial forces, so it must be balanced against the rigidity of thin-walled components. Final finishing passes with a fresh insert and a shallow depth of cut consistently deliver Ra 0.8 µm or better on titanium.
Practical Checklist for Titanium Turning
- Choose PVD-coated, sharp-edge carbide inserts designed for heat-resistant alloys.
- Start at conservative surface speeds (30–60 m/min) and adjust from tool life evidence.
- Never let the tool dwell; keep a constant, adequate depth of cut.
- Use high-pressure coolant aimed at the cutting edge.
- Stabilize part temperature before finishing passes.
- Inspect tool wear frequently — flank wear accelerates quickly once it starts.
Partner With a Shop That Has Machined Titanium at Scale
Titanium machining rewards experience, and it is a large part of our daily work at Hold-Tech Precision Industrial. Our team machines titanium and other heat-resistant alloys for aerospace, medical, and energy customers, with documented in-process inspection and a disciplined quality system.
Send us your titanium part drawing or model and we will review the geometry, suggest a machining strategy, and quote it with realistic lead times. Email operator@hold-tech.cn or use the contact form on our website, and a project engineer will respond with a detailed review.